Showing posts with label 6-Sigma. Show all posts

Tuesday, 3 January 2017

Impact of more than one Constraint - 5

Alan Barnard (at the 2006 TOC-ICO conference) asked the question whether the simple Throughput per Constraint Unit rule is valid with 2 (or more) overloaded resources. Alan used Eli Goldratt’s P-Q thought experiment for his discussion. His question is important because it is common to see businesses reduce ‘excess’ capacities to balance (or almost balance) capacities. The practice often results in two) or more concurrent constraints or ‘almost’ constraints. Since 2006 I have observed several factories that wonder why their output collapses below the theoretical capacity of their (almost) balanced lines.

I plan to show that that the Throughput per Constraint Unit rule continues to be valid using the same P-Q thought experiment. I also want to discuss this result in relation to the real World – how should companies manage resource capacities.

I would like readers to follow Eli Goldratt’s recommendation that they solve the problems – before I provide the solution and before my discussion of results. The learning experience will be greater and readers should be better able to discuss and critique my conclusions. If you are familiar with the thought experiment you can jump to the second part of this article.

The key part of the article comes at the end when the solution used in the P-Q thought experiment is discussed in relation to REALITY. The thought experiment should not lead managers to an easy solution. The tool is useful but requires thought and care.


Reality


As Eli Schragenheim[1] says, “The problem is not mathematical, the problem is the assumption reality is linear.” AND, a second problem is the assumption that “reality is deterministic”.


The real World is of course quite different from our thought experiment. In a real situation, customers will not allow their suppliers to dictate what they buy. Customers will not wait to buy Q because we want to make sure all the P demand has fulfilled (the original P-Q experiment). In reality we are unlikely to ever achieve the optimum. This is especially so when you consider that a business does not sell just 2 products, but more likely in the hundreds if not thousands of products. So forget about ever reaching the optimum.


BUT, is it still possible to move sales in the direction of better constraint utilisation?


In a real example, a business protects their engineering constraint by favouring the sale of standard products requiring no engineering. Their second favourite products are those that require only a small amount of engineering. Their annual sales have always been, and still are, limited by engineering. However, since their sales focus has changed the maximum possible annual sales have increased and, in turn, the business has become more profitable. Added sales are realised without the need for added to operating expenses. All that happened is sales of those items that do not need (much) of the constraint have increased significantly – without creating a new second (interactive) constraint.


Another example of using the Throughput per Constraint Unit as a tool to help decide what to sell is the Aramid fibre business (Kevlar®, Twaron®, Technora® are examples of brand names). A wide variety of aramids are produced with different structures and different fibre strengths (different decitex or weight per 10’000meters). Not only do many different varieties exist; aramids are also used in many different applications like sailcloth, ropes, filtration, tires, brakes, protective clothing (bullet proof vests) and more. Prices will vary from application to application and, of course, the price per unit of weight varies according to the decitex of the product. Since the various applications are so different, the sales and marketing organisation is divided into profit centres – each competing for supply. All this would be no problem until the factory is sold out and product must be allocated to customers.


A business can allocate fairly – give everyone the same relative amount less than they need; a difficult thing to do since clients catch on quickly and will order more to protect their business. The aramid supplier can also look at his product line and favour those products with the highest Throughput per Constraint Unit. (There is a fair chance that the most favourable or unfavourable products are not those with the highest or lowest margins.) He can also use the situation to target those customers that pay the lowest price in terms of Throughput per Constraint Unit and raise prices in those markets; higher prices tend to reduce demand or the client realises that, higher prices are justified.


The sales organisation needs to know the situation in relation to Throughput per Constraint Unit. They cannot switch away from clients and markets or raise prices as easily as I write this, but they can have a tool to help decide what they should do; where they should focus their sales and pricing efforts for greatest benefit.


Throughput per Constraint Unit is a tool to help decide what to do. Other considerations are part of the decision – including things like the importance of certain clients. When multiple profit centres are involved the tool can help resolve which of the profit centres should get preferential supply.


Eli Schragenheims work to develop a decision support system may well become the tool for business managers to use. (see footnote.)


Conclusions


  1. The simple Throughput per constraint unit does not always work, so be very careful (think carefully) when you believe you should be using it.
  2. The 5 focusing steps remain an excellent guide to manage a business. They do not absolve management from some critical thinking about how to approach initiatives to increase sales or to improvement operations.
  3. Many companies, by trying to balance capacity for cost reasons, will often leave a lot of money on the table. Judging how much money is left on the table is not an easy task. It is easier to decide to have just one constraint and to decide where the constraint should be. The lost sales, Throughput and profit due to balanced capacity can far outweigh the additional cost for just one constraint or even the additional cost to move the constraint into the market.
  4. Throughput and the impact of decisions on Throughput should take precedence over thinking about and taking actions to manage (reduce) inventories and/or cost. (A business is here to make money, not to save cost. If you want to save cost, do not start a business!) BTW – that Throughput should take precedence does not mean inventories and operating expense are unimportant.
  5. To think about what to sell (what to favour when selling) is a discussion that involves most of a business. Finance and controlling should lead the discussion. Sales and production are key participants. The managing director should probably also participate – after all some pretty key decisions will be proposed and made during such a discussion. To do this, scenarios must be built based on experience, knowledge and intuition about the constraining elements and the direction and opportunities in market demand. Such scenarios can be built and compared (see Eli Schragenheim’s work with his DSTOC software).
  6. So far the sales and operations planning process was not mentioned in the article; but this process, if it exists in the company, is a good place for such discussions. A good place as long as the appropriate participants are present, as S&OP design says they should be.


[1] Below are 3 article titles in relation to Eli Schragenheims thinking and his work in the area. They are found on his blog (https://elischragenheim.com/) that is well worth reading. Look for the following article titles: 1.) The Non-Linear Behavior of the Cost of Capacity; 2.) Is it really an opportunity? and 3.) The TOC Key Decisions Support (DSTOC).

Manicouagan Canoe Trip 16

After the portage around one of the waterfalls on the Manicougan River. ca. 1958 

Monday, 2 January 2017

Impact of more than one Constraint - 4


Alan Barnard (at the 2006 TOC-ICO conference) asked the question whether the simple Throughput per Constraint Unit rule is valid with 2 (or more) overloaded resources. Alan used Eli Goldratt’s P-Q thought experiment for his discussion. His question is important because it is common to see businesses reduce ‘excess’ capacities to balance (or almost balance) capacities. The practice often results in two) or more concurrent constraints or ‘almost’ constraints. Since 2006 I have observed several factories that wonder why their output collapses below the theoretical capacity of their (almost) balanced lines.

I plan to show that that the Throughput per Constraint Unit rule continues to be valid using the same P-Q thought experiment. I also want to discuss this result in relation to the real World – how should companies manage resource capacities.

I would like readers to follow Eli Goldratt’s recommendation that they solve the problems – before I provide the solution and before my discussion of results. The learning experience will be greater and readers should be better able to discuss and critique my conclusions. If you are familiar with the thought experiment you can jump to the second part of this article.

The key part of the article comes at the end when the solution used in the P-Q thought experiment is discussed in relation to REALITY. The thought experiment should not lead managers to an easy solution. The tool is useful but requires thought and care.

Interactive Constraints (like machines B and D in our example)

As we have just seen interactive constraints in my little PQ factory cut the maximum possible profit from 300€ per week to just 120€ per week (that is a 60% drop!). This is what interactive constraints can do to your business – they interfere with your capability to get the most from your most constraining resource.

Cost and efficiency pressures cause many business attempts to “balance” capacities – make all resources have about the same capability. This effectively introduces a second and potentially even more constraints into a production system. For most businesses, a collapse of capacity, is the surprising result – they cannot achieve even the original constraint’s capacity. Sales and profits are damaged. Not only do sales and profit suffer because current demand is not met; customers, because of poor delivery performance, leave for the competition, a much longer term loss and probably a much greater damage. 

To maximise profits and profitability most resources must have sufficient protective (or buffer) capacity so that capacity constraints cannot interact to damage the most constraining resource’s capability. Just one bottleneck is already one too many! Because, no matter what the supply chain does – when a demand spike occurs the company must either lose the added sales represented by the spike, or the company must promise delivery it cannot physically do. If a company promises what it cannot do, then the longer-term damage of lost clients will, sooner or later, happen.

To balance capacities is a ‘policy’ (or simply the way a company works). This ‘policy’ is a kind of (fake) constraint because the policy limits how much money the business can make. In such policy constraint cases; it is NOT this (fake) constraint the business must decide how to exploit (the 2nd step of the 5 focusing steps). The first step must be: change the faulty policy, including the faulty assumption that caused the business to balance capacities in the first place. Change the hidden assumption that resources are independent (operate in isolation) and therefore do not impact other (production) resources. A further assumption, not evident in the P-Q experiment is that resources are not subject to variability. Variability enhances negative effects caused by interactive constraints – if one breaks down the other constraints can easily be starved of work.

Observe this from the point of view of Lean and ask yourself this question: Does it make sense to reduce capacity/capability to balance capacity? Damaging your customers (because you cannot reliably supply) is a huge waste. Think about Lean as focused on maximising Throughput (and profit) and not focused first on minimising cost (waste). Consider lost Throughput as part of the waste you want to eliminate. The obstacle is managers do not view lost Throughput as waste. It is impossible for managers to put a “single definitive” number on Throughput waste – it’s an uncertain number dependent not only on what the company does, but also on client demand. On the other hand, cost ‘saved’ by firing a resource is a number you can easily determine – cost per person is in the ‘system’. (Never forget the impact firing a resource has elsewhere in your factory (because it can create interactive constraints). Also, remember how employees may react to the firing of their colleagues and friends to ‘balance’ capacities. How well will the remaining employees be motivated to help improve the business in the future?)

Observe this also from the point of view of Agile. We know that demand is uncertain, and often very uncertain at the article level. Ask yourself the question: Does it make sense to operate so close to capacity that any small spike in demand must be left to the competition to fulfil? Alternatively, does it make sense that we make promises to customers we cannot keep? To be agile means to be able to capture all demand our uncertain World sends our way. To do that we must be able to respond and capacity or capability is part of the answer.

Here is a second question: Does it make sense to keep a certain amount of protective capacity (“free” capacity) to be able to respond quickly? Protective capacity makes a company more agile, protects current Throughput and gives the business a better chance to gain new (more) Throughput.

You want your business to be Lean, but never anorexic. Lean means enough reserves to respond quickly and correctly to the changes our environment throws at it? Lean means having the stamina to win against your competitors. Anorexia will not do it.

This was some thoughts about interactive constraints and protective capacity. You may want to check out Eli Schragenheim’s blog for more about the importance of capacity buffers.


Manicouagan Canoe Trip 11

Manicouagan River Canoe Trip (1958?)  we slept under the canoes on that island … to avoid the black flies. The river is in Québec, islands like the one above are under water due to the Hydroelectric dams built since then.

Sunday, 1 January 2017

Impact of more than one Constraint -3

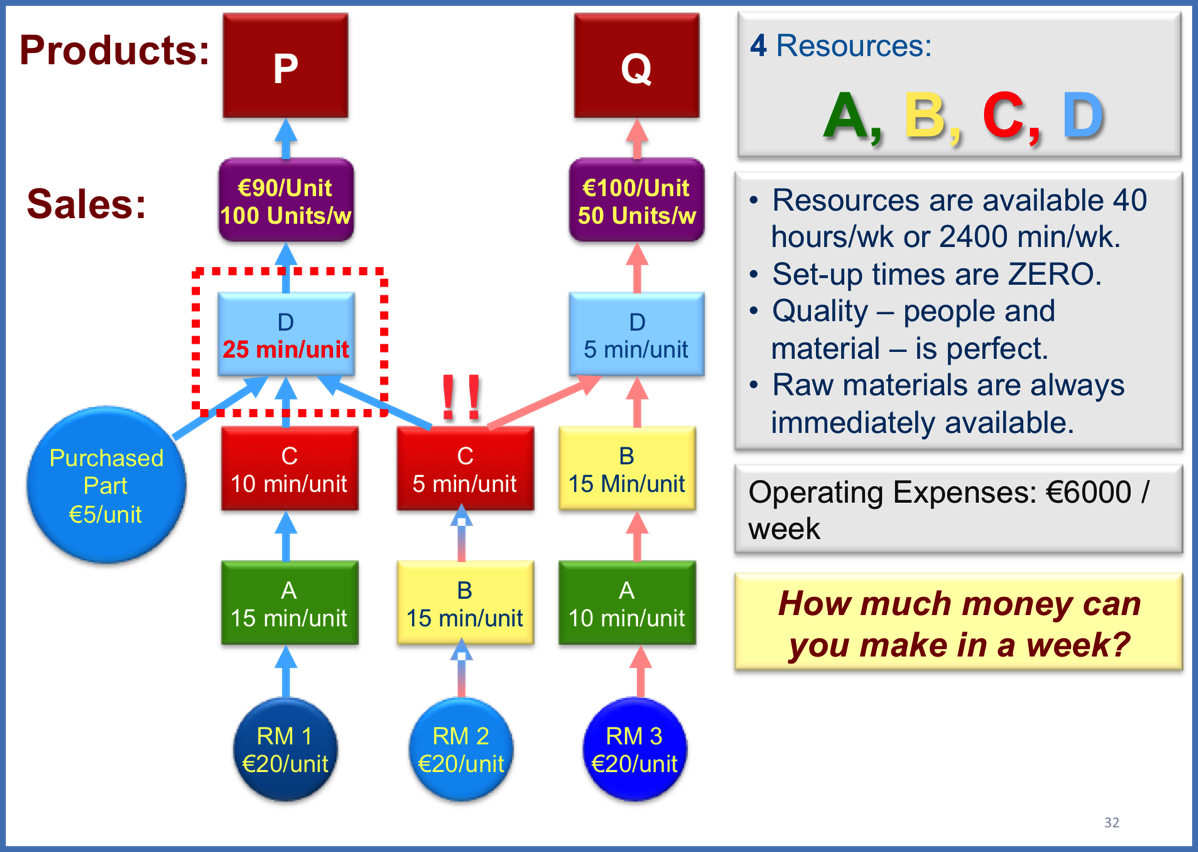
The P - Q thought experiment with 2 constraints


Alan Barnard (at the 2006 TOC-ICO conference) asked the question whether the simple Throughput per Constraint Unit rule is valid with 2 (or more) overloaded resources. Alan used Eli Goldratt’s P-Q thought experiment for his discussion. His question is important because it is common to see businesses reduce ‘excess’ capacities to balance (or almost balance) capacities. The practice often results in two) or more concurrent constraints or ‘almost’ constraints. Since 2006 I have observed several factories that wonder why their output collapses below the theoretical capacity of their (almost) balanced lines.

I plan to show that that the Throughput per Constraint Unit rule continues to be valid using the same P-Q thought experiment. I also want to discuss this result in relation to the real World – how should companies manage resource capacities.

I would like readers to follow Eli Goldratt’s recommendation that they solve the problems – before I provide the solution and before my discussion of results. The learning experience will be greater and readers should be better able to discuss and critique my conclusions. If you are familiar with the thought experiment you can jump to the second part of this article. 

The key part of the article comes at the end when the solution used in the P-Q thought experiment is discussed in relation to REALITY. The thought experiment should not lead managers to an easy solution. The tool is useful but requires thought and care.

Most of us ‘solve’ the problem without much thinking. It’s like a simple arithmetic problem from grade school. From groups we usually get quite number of ‘wrong’ answers – some from arithmetic mistakes, some from faulty thinking. Below you will find the answers from inadequate thinking and the explanation for the ‘right’ solution.

The only change in my little factory is the amount of time needed at D to produce 1 P. The time has increased from 15 to 25 minutes. Check it for yourself - both Band D machines have insufficient capacity to produce all the weekly demand.

NewImage


Below is the table showing how many minutes of each resource would be required to produce all the P and Q demand.


NewImage

Our simple rule to use Throughput per constraint unit is in difficulty – we have 2 constraints. But B is still the most constraining unit so lets try the rule. The table below shows the result.

NewImage

The rule does not seem to work. But we do have the more important rule that tells us to decide how to exploit the constraint (here we choose B, the more constraining resource). But to consume all the valuable B minutes we must have at least some D capacity available. So, we plan to sacrifice some P sales to liberate D capacity and make Q sales possible and to consume the primary (B) constraint’s capacity. B has 960 minutes of capacity available - enough to produce 32 Qs. To produce 32 Qs, I need 160 minutes; I must sacrifice 7 Ps.  BUT Sacrificing 7 Ps gives me 15 additional B minutes. I cannot use these to produce at the B machine (I need at least 30 minutes at B for 1 more Q).

Let’s sacrifice 8Ps and produce 36 Qs to consume all of B’s capacity – will our profits improve? Our secondary constraint (D) will still have 20 minutes of unused capacity after producing the 36 Qs.

NewImage


This looks good; but we still have 20 minutes of D capacity left with which we could produce up to 4 Qs. Lets produce just 1 more Q, which requires us to give up 2 Ps, but might increase profit.

NewImage

Not quite as good. 1 additional Q delivers 60€ more Throughput while giving up 2 of P costs 90€ Throughput – net we lose 30€ with every additional Q we produce. Not a good way to go. So lets try the other way – produce 1 more P.

NewImage

Also, not so good since we gain 45€ from 1 extra P but lose 60 from 1 less Q (net we lose 15€); AND we have 15 minutes of unexploited B left over. These 15 minutes would be enough for 1 added P. But by producing 1 P, we need 25 minutes of D capacity, which we no longer have. It looks like we have found the maximum profit possible, 120€/week.

By introducing a second constraint into the P-Q experiment the maximum possible is cut by more than 50%.

The rules to followed were

  1. Find the constraint (the most constraining resource).
  2. Decide how this resource is to be exploited.
  3. Subordinate everything else to that decision.

If we follow these 3 rules we should always find our way to the best mix to maximises our profit. (Alan Barnard used linear programming to find the same result.

In the next post I will discuss the impact of interactive constraints - like B and D are.


Cdn BaieComeau Oct 1955

Fall in the Canadian sub-arctic - near Baie Comeau Oct. 1955

Sunday, 19 April 2015

On Clear days you can see Corporate HQ 12

Why the 5 Focusing Steps are so Important

Most middle and senior managers do not understand or simply are not interested in how their business system works. They are content to focus on their local department and optimise that – rather than understanding the business as a whole to cause it to maximise results. Even top management (CEOs) often do not understand their business. They condone and even encourage their management teams to optimise their local departments – production, marketing sales, finance etc. Wherever local optimisation is the rule the business concerned will always harm the bottom line significantly. Local optimisation is a massive mistake!

The 5 Focusing Steps are guidelines that, properly used, will cause a management team to always reflect on their (local) decisions. Doe the action or decision taken locally help or damage the business as a whole? As we will see the 5 Focusing Steps are a guide, but they do not replace a deep understanding of the business system.

What follows is my fifth example of the impact of the exploit and subordinate steps on the bottom line. In this example I have chosen a situation in which top management has sent a directive to all factories to increase yields (reduce scrap rates). The factory managers’ bonus would depend on achieving the 3% improvement target. Just a small policy change would be worth a huge amount.

BTW. If you have any similar examples please share them with me. I will publish them (if there are not too many!) Send your stories to CSSTW@Bluewin.ch - I will credit you with the story.

5th Example of the 5 Focusing Steps in Action

Yield Increase or Scrap Reduction Targets

Every once in a while senior management comes up with a great idea. In this case the COO came up with the directive that all factories must increase yields by 3% (or reduce scrap rates by that amount). The directive was sent to all factories around the World. On the face of it a good idea.


Production management at one of the factories were convinced that their machines, very large machines, would not allow them to achieve their 3% improvement target. They made 3 standard colours in high quantities and a number of the colours of the rainbow in small quantities. The 3 major colours were no problem, yields were already excellent there - actually the problem was that no significant improvement was possible. These small quantities of colours suffer from poor yields (high scrap rates) because change-overs for small quantities on large machines consume a lot of material to be sure the colour from the previous lot has been fully flushed from the system.  The required quantities of pigmented products is not very high so that changeover material losses were a high percentage of production batches. The situation could also not be improved with their existing equipment - cleaning by dilution takes a lot of material.

The factory solved their problem by outsourcing pigmented production to suppliers that have smaller machines. They met their yield targets but as a consequence had quite long periods of no production on their big machines when they would normally be producing colours and, of course, they had to pay considerable fees for the outsourced production.

After a year the business manager was transferred elsewhere. The new manager saw the damage caused by the outsourcing. What he saw was an annual net penalty if 1.5 million$ (the cost of outsourcing far outweighed the value of any yield gains).

Here we have another example of a damaging corporate policy that should have never been implemented in the factory concerned … and possibly also elsewhere. Improved yields are a good target to set but should be done with full knowledge of any consequences. In fact senior managers (COOs) should allow (in fact expect) their managers to raise such potential negative outcomes of an action. If they did allow/expect such reactions, then many businesses might be better off.
BaieComeau Ruedi Susi August 1953 01

Monday, 6 April 2015

On Clear days you can see Corporate HQ - 10

Why the 5 Focusing Steps are so Important

Most middle and senior managers do not understand or simply are not interested in how their business system works. They are content to focus on their local department and optimise that – rather than understanding the business as a whole to cause it to maximise results. Even top management (CEOs) often do not understand their business. They condone and even encourage their management teams to optimise their local departments – production, marketing sales, finance etc. Wherever local optimisation is the rule the business concerned will always harm the bottom line significantly. Local optimisation is a massive mistake!

The 5 Focusing Steps are guidelines that, properly used, will cause a management team to always reflect on their (local) decisions. Doe the action or decision taken locally help or damage the business as a whole? As we will see the 5 Focusing Steps are a guide, but they do not replace a deep understanding of the business system.

What follows is my third example of the impact of the exploit and subordinate steps on the bottom line. In this example I have chosen a situation in which there is a constraint only during a part of the year - that could be overcome through inventory management. Just a small policy change would be worth a huge amount.

BTW. If you have any similar examples please share them with me. I will publish them (if there are not too many!) Send your stories to CSSTW@Bluewin.ch - I will credit you with the story.

3rd Example of the 5 Focusing Steps in Action

Year-end Low Inventory Targets

Such targets are policies instituted to demonstrate a well-managed business with low inventories to Wall Street and investment analysts. Factory and business managers are given no choice but to meet these year-end targets no matter the problems it gave the business.
One business always met its targets with the full knowledge that as soon a January starts they would not be able to fulfil market demand. Because they could not deliver everything early in the year they were later forced to lower prices in order to win back the lost business. Year-end inventory targets were extremely damaging to their bottom line. A 1% price reduction cuts a 10% margin by 10% to 9%. Can you imagine that 1% is enough price incentive to win back customers?
0T2 5 Steps
Another business, also with a stringent year-end inventory target, sold synthetic yarns to a special industry that created fabrics for the consumer market. The nature of this business was such that during the first quarter of every 2 years out of 3, demand would exceed supply by a considerable amount. Since year-end inventory targets were holy, factory management did not dare to produce for the first quarter. Instead the produced enough for the first quarter but sold the extra amount (above inventory targets) to dealers at very low prices – at least this way their customers would be satisfied – they get the quantities they need from their factory  and not from competitors. 
Calculate for yourself what the cost would be to hold the extra inventory for on average 5 months 2 years out of 3 and say 8 months in years without peak demand. The cost of holding the extra materials is minimal compared to the extra income (Throughput). The extra income is sales less materials cost.
Factory management was most irritated by this because the dealers owned Aston Martins and Ferraris while they (factory management) could only afford Fords!
Clearly, when you read these 2 examples the conclusion has to be that the policy concerned is not a good one. Low inventories are certainly a good idea, but only once you can continue to meet demand despite low stock levels. Corporate management is the problem. What they want is fine, but it should not be requested equally from all factories. A further problem is it is very difficult to get sufficient time with top managers (either because these are too busy or middle managers fear for their careers) to show that the local optimisation of inventory leads (in such cases) to bottom line damage. Such situations often live on for many years damaging the company year after year.

IMG 0574

Sunday, 5 April 2015

On Clear Days you can see Corporate HQ - 9

Why the 5 Focusing Steps are so Important

Most middle and senior managers do not understand or simply are not interested in how their business system works. They are content to focus on their local department and optimise that – rather than understanding the business as a whole to cause it to maximise results. Even top management (CEOs) often do not understand their business. They condone and even encourage their management teams to optimise their local departments – production, marketing sales, finance etc. Wherever local optimisation is the rule the business concerned will always harm the bottom line significantly. Local optimisation is a massive mistake!

The 5 Focusing Steps are guidelines that, properly used, will cause a management team to always reflect on their (local) decisions. Doe the action or decision taken locally help or damage the business as a whole? As we will see the 5 Focusing Steps are a guide, but they do not replace a deep understanding of the business system.

What follows is my second example of the impact of the exploit and subordinate steps on the bottom line. In this example I have chosen another situation in which a there is apparently a clear physical constraint in the factory concerned. However through just a few simple changes to the way the factory works in relation to the constraints (policy changes) they also were able to move from an overloaded situation to being able to meet all demand with the expected lead time.


BTW. If you have any similar examples please share them with me. I will publish them (if there are not too many!

2nd Example of the 5 Focusing Steps in Action

Exploiting the constraint in a coatings (for automotive) factory

Before I arrived at the factory I knew that factory management was lobbying for more vessels to hold paint. They claimed their constraint was the number of storage vessels; they had already submitted a project to install 2 additional vessels.

0T1 5 Steps

This time I ran a simple simulation to show the impact of properly exploiting the constraint. Participants were supervisors from the factory and plant management. The simulation went well, the people got the idea and began discussing the constraint. I did not believe the constraint was the vessels since I also knew that quality control had limited capacity due to illness and an accident that reduced capacity by a large amount. Because evaluating colour takes several years to learn adding people to quality control was not going to work.

I led the team to the idea that quality control is the constraint of the system. Initially they were doubtful but when they began to think about the quality control job and the amount of time actually spent evaluating colours it became clear that quality control, even with 2 of their 4 people out of action, had enough capacity to do the job of colour quality control correctly. The decision made was that the colour experts would do only colour evaluations. To collect samples they would no longer walk back and forth between the lab and the factory; they would no longer add the corrections to the mix vessels and they would not wait until mixing was complete. Other employees were found to make the corrections (weighing pigments and adding these to the mixing vessels), people were found to collect samples and the quality control experts found ways to reduce the number of corrections needed. All these actions were "subordinate to the constraint” actions – subordinate to decision that the two colour experts in QA would focus only on colour evaluations.

Once all the actions the team decided were implemented the factory enjoyed a 40% increase in capacity – and no longer needed to buy any added vessels.

IMG 0420

On Clear Days you can see Corporate HQ - 8

Why the 5 Focusing Steps are so Important

Most middle and senior managers do not understand or simply are not interested in how their business system works. They are content to focus on their local department and optimise that – rather than understanding the business as a whole to cause it to maximise results. Even top management (CEOs) often do not understand their business. They condone and even encourage their management teams to optimise their local departments – production, marketing sales, finance etc. Wherever local optimisation is the rule the business concerned will always harm the bottom line significantly. Local optimisation is a massive mistake!

The 5 Focusing Steps are guidelines that, properly used, will cause a management team to always reflect on their (local) decisions. Doe the action or decision taken locally help or damage the business as a whole? As we will see the 5 Focusing Steps are a guide, but they do not replace a deep understanding of the business system.

What follows is a first example of the impact of the exploit and subordinate steps on the bottom line. In this the first example I have chosen a situation in which a there is a clear physical constraint in the factory concerned. However through just a few simple changes to the way the factory works in relation to the constraints (policy changes) they were able to move from an overloaded situation to being able to meet all demand with the expected lead time.

Examples of the 5 Focusing Steps in Action

Exploiting the constraint in automotive component production

The factory produces a major component for both cars and trucks. Production involves a series of steps followed by an automated assembly and lastly some manual final assembly. The company invited me to a meeting with the plant manager to discuss how TOC (and the 5 Steps) could solve his problem of insufficient capacity.

The plant manager's problem was demand far exceeded the factories capability to supply (by about 25%). Instead of a discussion with the him, he confronted me with 16 sceptical engineers who had been working on the problem already for a very long time.

0T0 5 Steps

I explained the 5 steps and their importance. This led to a discussion about the location of their constraint. With 16 engineers in the room consensus was difficult. After a while it became clear that they believed either a metal turning step or the final manual assembly step were the possible constraints. I explained that it is unusual to find the constraint at the end of a production line simply because month end pressures to meet sales targets ensure plenty of capacity there. They finally agreed that the best candidate was the turning machine in a line (they had 10 lines).

From there it was easy. I asked them how many hours per day the constraint machines would be producing. They claimed constantly except for set-ups. I asked to see these machines. We went to 5 lines and found that in 3 of them (60%) the turning machine was idle. They were idle for set-ups (but no set up person was present) and one was idle for a break. Clearly they were losing capacity at the constraint and therefore for the factory.

Back in the conference room the engineers came up with many ideas to make sure the constraint never stops (apart from actual work doing set-ups). They also came up with ways to accelerate set-ups significantly. Most of the changes could be made immediately (some did require the OK from their union). The result was they easily discovered the 25% of capacity needed to meet demand!

To exploit the constraint they had to find ways to shorten set-ups; they had to find ways to cover for breaks, meals and shift changes and they eventually found ways to move material between production lines since the constraint was not equally loaded across all 10 lines.

IMG 0353


Friday, 3 April 2015

On Clear Days you can see Corporate HQ - 7


Why the 5 Focusing Steps are so Important

Most middle and senior managers do not understand or simply are not interested in how their business system works. They are content to focus on their local department and optimise that – rather than understanding the business as a whole to cause it to maximise results. Even top management (CEOs) often do not understand their business. They condone and even encourage their management teams to optimise their local departments – production, marketing sales, finance etc. Wherever local optimisation is the rule the business concerned will always harm the bottom line significantly. Local optimisation is a massive mistake!

The 5 Focusing Steps are guidelines that, properly used, will cause a management team to always reflect on their (local) decisions. Doe the action or decision taken locally help or damage the business as a whole? As we will see the 5 Focusing Steps are a guide, but they do not replace a deep understanding of the business system.

What follows is a discussion of the impact of the exploit and subordinate steps on the bottom line. If an organisation follows the 5 steps correctly they can easily find 20 - 40% greater Throughput. The impact of the exploit decision and subordination is shown using several cases (materials cost at 35%, 50% and 65% of sales and 10, 20 and 30% positive impact on sales.

Why are the 5 Steps so Important for a Business

The decision to exploit and subordinate to the constraint

Consider a business with an internal constraint. The constraint limits how much can be produced and sold. This business now applies the 5 focusing steps. As a result, without adding any fixed costs, the business finds it can sell 10, 20 and 30% more (gains that can often be easily achieved). The tables below show the impact in 3 different situations – one with 35% material cost; one with 50% material costs and one with 65%. In all 3 cases the businesses earn 5% on sales (profit is 5% of sales).
1010 35


With low materials cost (35%) the leverage is huge. 
1010 50


Despite less leverage with higher materials costs the impact is still impressive.
1010 65


With very high materials (totally variable costs) the leverage declines further but a good impact remains.
From the 3 tables it is clear that following the 5 Steps can have a very significant positive impact on the bottom line. Someone wishing to use the 5 Steps faces the problem that current experience tells managers that such impact is just not possible. They cannot believe that such huge jumps in profitability are possible after their many years of improvement initiatives. The claim insults their capability and their view of themselves as successful managers. The examples below, taken from real life situations, will hopefully demonstrate the possibilities and the pitfalls of not following the 5 steps. (Nevertheless there will always be resistance; much of which in the form of ‘we are different’.)

Elevating or expanding the constraint

After following the 5 Steps in a disciplined way the organisation will know exactly where to expand. The expansion will immediately lead to more sales and Throughput. If in the above first example I have 3 resources machines in my constraint area then a new resource can potentially add 25% to sales and Throughput for a small amount of added costs. It is of course essential to know the cost of such an expansion since you may have to expand the near constraints too or the sales organisation may be unable to increase sales.
The decision how to exploit the constraint and proper subordination has the biggest impact on the bottom line. It’s free! Following the 5 steps correctly and continually is the most rewarding action an organisation can take. It focuses scarce improvement resources at the point of greatest rewards – great for the company and very motivating for the improvement team.
IMG 0578

On Clear days you can see Corporate HQ - 4

Why the 5 Focusing Steps are so Important

Most middle and senior managers do not understand or simply are not interested in how their business system works. They are content to focus on their local department and optimise that – rather than understanding the business as a whole to cause it to maximise results. Even top management (CEOs) often do not understand their business. They condone and even encourage their management teams to optimise their local departments – production, marketing sales, finance etc. Wherever local optimisation is the rule the business concerned will always harm the bottom line significantly. Local optimisation is a massive mistake!

The 5 Focusing Steps are guidelines that properly used will cause a management team to always reflect on their (local) decisions. Is the action or decision taken locally help or damage the business as a whole? As we will see the 5 Focusing Steps are a guide, but they do not replace a deep understanding of the business system.

What follows is a description of the 5 focusing steps, how to apply them, why each step is important and a series of examples of common practice that violate the 5-Steps. This fourth post is a short discussion of the third (probably the most difficult to implement) of the 5 steps.

The 5 Focusing Steps

Step 3; Subordinate Everything Else to the Decision how to Exploit

This is the difficult step. Imagine that sales are asked to sell lower margin products (in preference to higher margin ones). The fact is that our lower margin products consume our constraint (equipment) resource more effectively; that we get many more low margin products per unit of time from our constraint is a good reason to favour these. Sales, if they are measured by price or margins may well resist such subordination.
Similarly production generally loves big batches or efficiency at every resource. At first glance the right way to go, but big batches extend lead-times of those products waiting their turn. Long lead times (due to big batches, compromise quality - quality control sees problems much later. This quality issue tends to cost in other ways too - materials cost increases and capacity is reduced. The focus on efficiency everywhere wastes scarce improvement resources that should focus efforts on the limiting factor – our constraint.
These examples show how difficult it is to get the correct behaviour. Departments and their managers are measured and rewarded by the results of just their department and not by the effect these managers have on the business as a whole. True, some corporations have a bonus system that rewards middle managers by the overall results. This is a first step, but an ineffective one.
Bosses are used to measuring their employees by the results they achieve locally mainly because they do not have the tools to measure impacts their people have on the business as a whole.
Every business has a lot of work to do to give their managers and employees the information necessary to properly subordinate to the constraint. The data is there in ERP systems; it just needs to be transformed into information!
Part of my garden!
Jardin Burkhard

Friday, 27 March 2015

Economic Order Quantity (EOQ)

EOQ is a Cost World metric. The purpose of the method is to find the minimum cost of buying and holding inventory. It does not take into consideration the impact inventory has on Throughput (and sales). Too low (and the wrong) inventory will almost certainly cause a company to lose sales, Throughput and profit.

The reason to minimise inventory should not be to minimise these to costs. It should be to minimise lead-times (for low inventories in a supply chain, lead-times must be low). The shorter lead-times are the smaller the bullwhip effect and the smoother demand will be on production. The smoother demand on production is, the more effective production will be in on time delivery, ensuring product availability, production capability (capacity to produce) and production cost per unit.

In the TOC World we focus on maximising Throughput which, done correctly, leads to the lowest overall cost. We focus on placing inventory in the right place in order to ensure due date and availability near 100%. We focus on minimal lead-times to minimise the bullwhip effect and thus also inventory. Because of this focus it can easily happen that TOC Throughput tactics take an organisation away from the EOQ minimum – often towards the left with more frequent re-ordering.

So, is EOQ a valuable concept? Or, is it dangerous?

IMG 0394

Thursday, 6 January 2011

Project Managers Risk Averse? - Part IX

There are many stories of projects where 90% of the project takes 100 days and the last 10% also take 100 days. Too often project managers and top management get significant surprises late in the project. Could these surprises be known about earlier? What needs to be done to get the appropriate information? If we can get the information risk will be less.

9. Minimize Risk; Early Warning

Common practice, as discussed earlier, is to get a commitment from resources performing tasks. They try their best to make commitments that gives them a high chance of finishing their task(s) on time.

During execution it is not really ‘polite’ to ask for progress in tasks that have just started – after all the task is not due yet and the project manager has a commitment. So, at least early on during a task there is no report on progress – and therefore no knowledge of a possible problem.

When a task is planned the task owner must make assumptions about the task and his environment (for instance the number of tasks he has). When a resource starts work on a task he soon knows how long the task will take with much greater accuracy than at the time he made his estimate for the project plan. Why don’t project managers get this information and use it to help manage their projects better?

How about applying the following tactics. Instead of reporting completion progress e.g. a task or project is 25% complete let’s request the time remaining in tasks. All resources report how many more days they need to complete their task. That way (if they make an honest evaluation) the project manager knows immediately when a problem arises – rather when it is already to late from saving the project from missing its due date. (Remember cutting scope, or spending more money are the equivalent of missing the due date.)

There is the question of what to report and how frequently. Since project managers want early warning, report frequency must be high – say daily. To achieve such a frequency reporting must not be onerous. If only resources with started tasks report and all they report is the expected remaining task time, is that onerous? If WIP and multi-tasking have been reduced, then there will be fewer tasks to report and knowledge over remaining time will be better.

Does this make sense? Will this give the project manager a better view of the status of their project? Will it give top management a better view of their portfolio of projects?

What are the obstacles to implementation?

<

Technorati Tags: , , , , , , , , , , , , , , , , ,

/p>

Individual and Tribal Behaviour

I have been a proponent of the Theory of Constraints (TOC) for many years now and still it is very difficult to ‘sell’ TOC to business people around the World – despite agreement that everything in TOC makes eminent sense. My friends in the TOC community experience the same things. That something new is a difficult sell is nothing new. Just read about the difficulties all sorts of inventors have had.

Confirmation Bias

Your personal experience should tell you that young liberal and open people are likely to believe that marijuana is harmless. You see them read or watch information about marijuana and retain only the positive (marijuana is not dangerous) parts of the presentation – even if the article or TV show is totally balanced for or against.

On the other hand the older, conservative (in relation to marijuana) less open person will do the exact opposite – he will retain only what confirms his existing views.

Both parties are exhibiting ‘confirmation bias’ – people everywhere seek out those things that confirm their preconception and tend to ignore contrary opinions, arguments and facts.

Look at your own behaviour. You and your partner have an argument about something. Try and notice how you respond to the facts, opinions and arguments put forward by others – which do you truly consider. D you really look at and logically think through the other positions? Or do you reject them quickly. What does it feel like when you suddenly realize your partner is correct – you are about to lose the argument?

As a proponent of the Theory of Constraints and as a human being I must behave in a similar way when confronted by other improvement methodologies. Lean, TPS and 6-Sigma experts must be similar, but they have a different bias.

In fact all of these improvement philosophies have a lot to offer, but this confirmation bias is getting in the way of progress and constructive discussion – at last many times.

The book “RISK The Science and Politics of Fear” by Dan Gardner discusses confirmation bias and many other topics of interest.

Tribes (Culture)

We are all members of tribes. I am a member of the TOC tribe; you might be a member of the Lean or 6-Sigma tribe. Within each tribe there are a series of (un-)spoken rules and expected behaviours. In the TOC community many of us look to Eli Goldratt for guidance (even if he wishes us to THINK on our own). Some try to emulate our leader. Some simply follow the generally accepted practices and thoughts of the community as a whole. As long as you conform you have the support of the community. If you don’t you run the risk of being ostracized by the group. This tribal behaviour means that many of us cannot accept Lean, 6-Sigma etc. We even have more explanations why these other methods are ‘wrong’ rather than looking for the good.

Other improvement methodologies probably react in similar ways – so it takes a very long time to get an integrated even more powerful toolset that incorporates the best from each. (Goldratt in his article ‘Standing on the Shoulders of Giants’ tries to show the way. However even this article must cause other tribes (other than the TOC tribe) to react less than positively.)

What we are experiencing is tribal behaviour – we are protecting our own community, our ideas etc. Given tribal behaviour and confirmation bias it is amazing that a coming together happens at all!

I would like to invite everyone that reads this to join the TLS group on Linkedin. TPS stands for Theory of Constraints, Lean and Six-Sigma. I would like to invite you all to join the TLS - TOC Lean & Six Sigma group in Linkedin. (I am a member, but not the group’s owner)

For more on tribal behavior read “Great Boss-Dead Boss” by Ray Immelman

The Challenge for ALL of Us

  • How can we cause the various improvement methodology communities to integrate? How can we improve management processes far beyond where they are now? How can we foster real discussion and avoid confirmation bias?
  • How can we create one CI (Continual Improvement) tribe that encompasses 6-Sigma, Lean, TOC and whatever else is out there or about to come on the scene?
  • How can we speed up progress without the risk of embracing something truly wrong and risky?

<

Technorati Tags: , , , , , , , , ,

/p>